How to Choose a Thermoforming Mold Assembly?
Choosing a Thermoforming Mold Assembly is not a simple matter of selecting steel, aluminum, or epoxy. The decision affects cycle time, part accuracy, cooling performance, maintenance, and final surface quality. A mold may look impressive on a drawing, yet perform poorly when vacuum paths clog or cooling channels leave hot spots.
Dr. James L. Throne, a recognized thermoforming authority, described the process as “heating a thermoplastic sheet to its softening temperature, forming it against a mold, and trimming it.” His statement highlights the real challenge: heat control is central to mold selection. A suitable Thermoforming Mold Assembly must support consistent heating, controlled forming, reliable cooling, and clean release. Small details matter. Vent holes near deep corners can prevent webbing. Evenly spaced cooling channels can reduce warpage around thick ribs. A polished surface can improve appearance, but it may also expose scratches more clearly.
This guide examines the practical questions behind each choice. What material suits the production volume? How complex is the part geometry? Can the mold be repaired without long downtime? Are interchangeable inserts worth the added cost? There is no universal answer. Sometimes, a lower-cost mold seems efficient, but repeated trimming defects may erase the saving. Sometimes, an advanced assembly is unnecessary for a short trial run. That is where judgment becomes important. Real production conditions often challenge the original design. Careful testing, documented results, and honest review should guide the final decision.
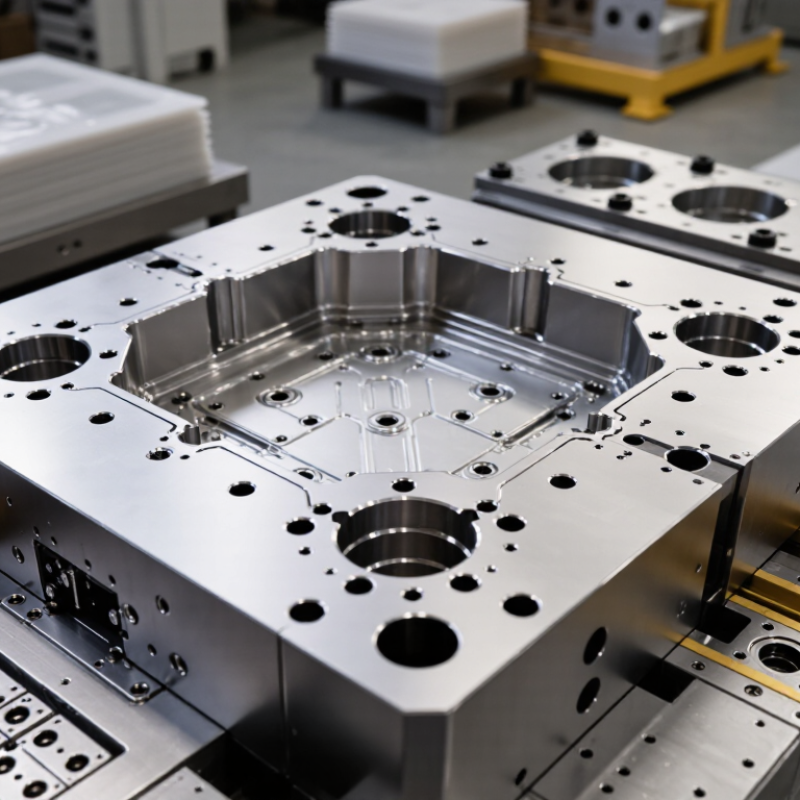
Define Part Requirements: Material, Thickness, Draw Ratio, and Production Volume
Choosing a thermoforming mold assembly starts with the part, not the machine. Material behavior sets the heating window, cooling demand, and release strategy. ABS, PET, PP, and recycled blends can require different venting and shrinkage allowances. PlasticsEurope’s Plastics—The Fast Facts 2024 reports that packaging remains Europe’s largest plastics-use sector, at about 40% of demand. That volume increases pressure for stable cycles and repeatable wall thickness.
Thickness and draw considerations Thickness must be checked at corners, ribs, and the deepest draw. A nominal 1.5 mm sheet may become dangerously thin near a sharp base. Draw ratio helps expose this risk. A practical estimate divides the cavity depth by the smallest projected opening dimension. High ratios may need plug assistance, pre-stretching, generous radii, or a different mold assembly. Poor vent placement can leave small shiny patches, trapped air, and incomplete detail. They are easy to miss.
Tooling and production volume Production volume changes the tooling decision. Low-volume work may justify aluminum tooling with simpler cooling. High-volume production usually needs stronger temperature control, replaceable wear parts, and faster mold changeover. The Plastics Industry Association’s 2023 Size and Impact Report describes the U.S. plastics industry as a major manufacturing sector with millions of jobs, yet productivity still depends on disciplined process control. In practice, I would test the actual sheet, not only its datasheet. Material batches vary. Our first design may still be wrong. A short trial can reveal more than a confident calculation.
Select Mold Architecture and Materials: Aluminum Delivers 167–205 W/m·K
Choosing a thermoforming mold assembly starts with its architecture, but material selection controls daily production stability. Aluminum typically offers thermal conductivity between 167 and 205 W/m·K, depending on alloy, temper, and temperature. This range supports faster heat transfer than many steel alternatives. In practical trials, an aluminum mold can cool sheet surfaces more evenly and shorten cycle adjustments.
Mold geometry still matters. Deep cavities, narrow corners, and uneven wall thickness can create local hot spots. A well-designed cooling channel should follow these demanding areas closely. I usually inspect temperature readings across the cavity, not only at the inlet and outlet. Small differences can become visible marks, warping, or inconsistent forming.
Aluminum is also easier to machine for prototypes and medium-volume tooling. It is not automatically the perfect choice. The alloy must resist wear, distortion, and repeated thermal cycling. Thin walls may require reinforcement, while aggressive cleaning methods can damage the surface finish.
I would verify conductivity with supplier data and confirm it through shop-floor testing. One overlooked issue is thermal expansion. Mold alignment may shift slightly as the tool heats. That detail deserves attention. Engineers should compare cooling performance, expected production volume, surface requirements, and repair plans before approving the assembly. Sometimes a simpler mold with better temperature control outperforms a more complex design.
Set Process Parameters: 0.8–0.95 bar Vacuum and 10–60 s Cycle Time
How to Choose a Thermoforming Mold Assembly?
A mold assembly should match the forming pressure, material, and cooling demand. For vacuum forming, target 0.8–0.95 bar vacuum under stable conditions. This range creates strong sheet contact with detailed mold surfaces. However, 0.95 bar is not automatically better. Poor vents can still trap air and create webbing.
PlasticsEurope’s Plastics – the Facts 2023 reports global plastics production reached 400.3 million tonnes in 2022. Packaging remained the largest application sector. This volume increases pressure for repeatable, material-efficient forming. Select aluminum or temperature-resistant tooling when heat removal matters. Use evenly distributed vacuum channels, not only one central port. A 10–60 second cycle can work, but cycle time depends on sheet thickness, polymer grade, mold temperature, and cooling airflow. Thin sheets may release quickly. Thick parts often need longer cooling.
Tips: Measure vacuum at the mold, not only at the pump. Check leakage before production. Record forming temperature and release time for every trial. Keep vents clean and short. A simple test part can reveal more than a perfect spreadsheet. I would also challenge the planned cycle time after production starts. Faster cycles may increase warpage, stress, or incomplete detail. Leave a small process window for seasonal temperature changes and operator variation.
Verify Mold Fit: Machine Area, Clamping Force, Draft, and Venting Standards
Choosing a thermoforming mold assembly starts with a physical fit check, not a catalog image. Measure the machine area, including the frame, heater clearance, and moving platen limits. A mold can fit the table yet collide with nearby hardware. Leave access for cleaning and inspection. Small oversights become expensive delays.
Clamping force must match the projected forming area and the process pressure. Use the machine manual, material data, and verified production records when calculating the load. Add a practical safety margin, but avoid excessive force that may damage the mold or platen. I have seen early estimates fail because trim waste was included incorrectly. Recheck the calculation with actual part dimensions. The result should be documented, not remembered.
Draft angles should release the formed part without scuffing vertical walls or stretching corners. Deep features usually need more draft, especially when cooling shrinkage increases grip. Venting also deserves a measured design. Place fine vent paths near corners, deep pockets, and surface details, then confirm their size against the material and wall thickness. Blocked vents can leave cloudy marks or incomplete details. A production trial may reveal uneven vacuum flow that drawings miss. That result should lead to a mold adjustment, not an excuse. Keep records of mold fit, clamping force, draft checks, and venting performance for repeatable approval.
Validate Performance: Cooling Uniformity, Tolerances, Tool Life, and Cost
How to Choose a Thermoforming Mold Assembly? Validate cooling uniformity before judging price. PlasticsEurope’s Plastics—The Fast Facts 2024 reports 413.8 million tonnes of global plastic production in 2023. That scale magnifies small process losses. A mold with uneven water channels can create hot corners, uneven wall thickness, and visible warpage. Measure each circuit’s inlet and outlet temperature, flow rate, and pressure. Use thermal imaging during production trials. Do not guess.
Tolerances should match the part’s function, not an impressive drawing. ISO 20457 provides guidance for tolerances in plastics manufacturing, but actual results depend on material shrinkage, sheet temperature, and machine stability. Record cavity dimensions at operating temperature. Cold measurements can mislead. A practical target is consistent thickness across critical zones, verified through sectioned samples and capability studies. Perfect uniformity is unlikely. That deserves honest review.
Tool life depends on cooling, steel selection, surface treatment, and maintenance access. The U.S. Department of Energy’s Industrial Decarbonization Roadmap identifies plastics processing as an important energy-consuming manufacturing sector, making efficient cooling worth measuring. Compare total cost, not purchase price. Include machining, water treatment, cycle time, rejected parts, and planned refurbishment. A cheaper assembly may become expensive after repeated leaks or long changeovers. I would also challenge the first design after testing; production often exposes assumptions that CAD cannot.
How to Choose a Thermoforming Mold Assembly? — Validate Performance
Representative engineering comparison of cooling uniformity, dimensional tolerance, tool life, and relative tooling cost. Higher scores indicate better overall performance for each criterion.
| Mold Assembly | Max Surface ΔT | Typical Tolerance | Expected Tool Life | Relative Cost Index |
| Conventional drilled aluminum | 8.0 °C | ±0.10 mm | 50,000 cycles | 1.0× |
| Cast aluminum | 5.0 °C | ±0.15 mm | 30,000 cycles | 0.8× |
| Conformal-channel aluminum | 2.5 °C | ±0.08 mm | 80,000 cycles | 1.5× |
| Machined steel | 4.0 °C | ±0.05 mm | 200,000 cycles | 2.5× |
Cooling uniformity is represented by the maximum temperature difference across the forming surface; lower values reduce uneven shrinkage and warpage. Tolerance reflects typical machined or formed dimensional capability, while tool life depends on material, operating temperature, abrasion, maintenance, and production conditions. The cost index uses conventional drilled aluminum as the 1.0× reference, so final quotations should be validated with tooling suppliers.